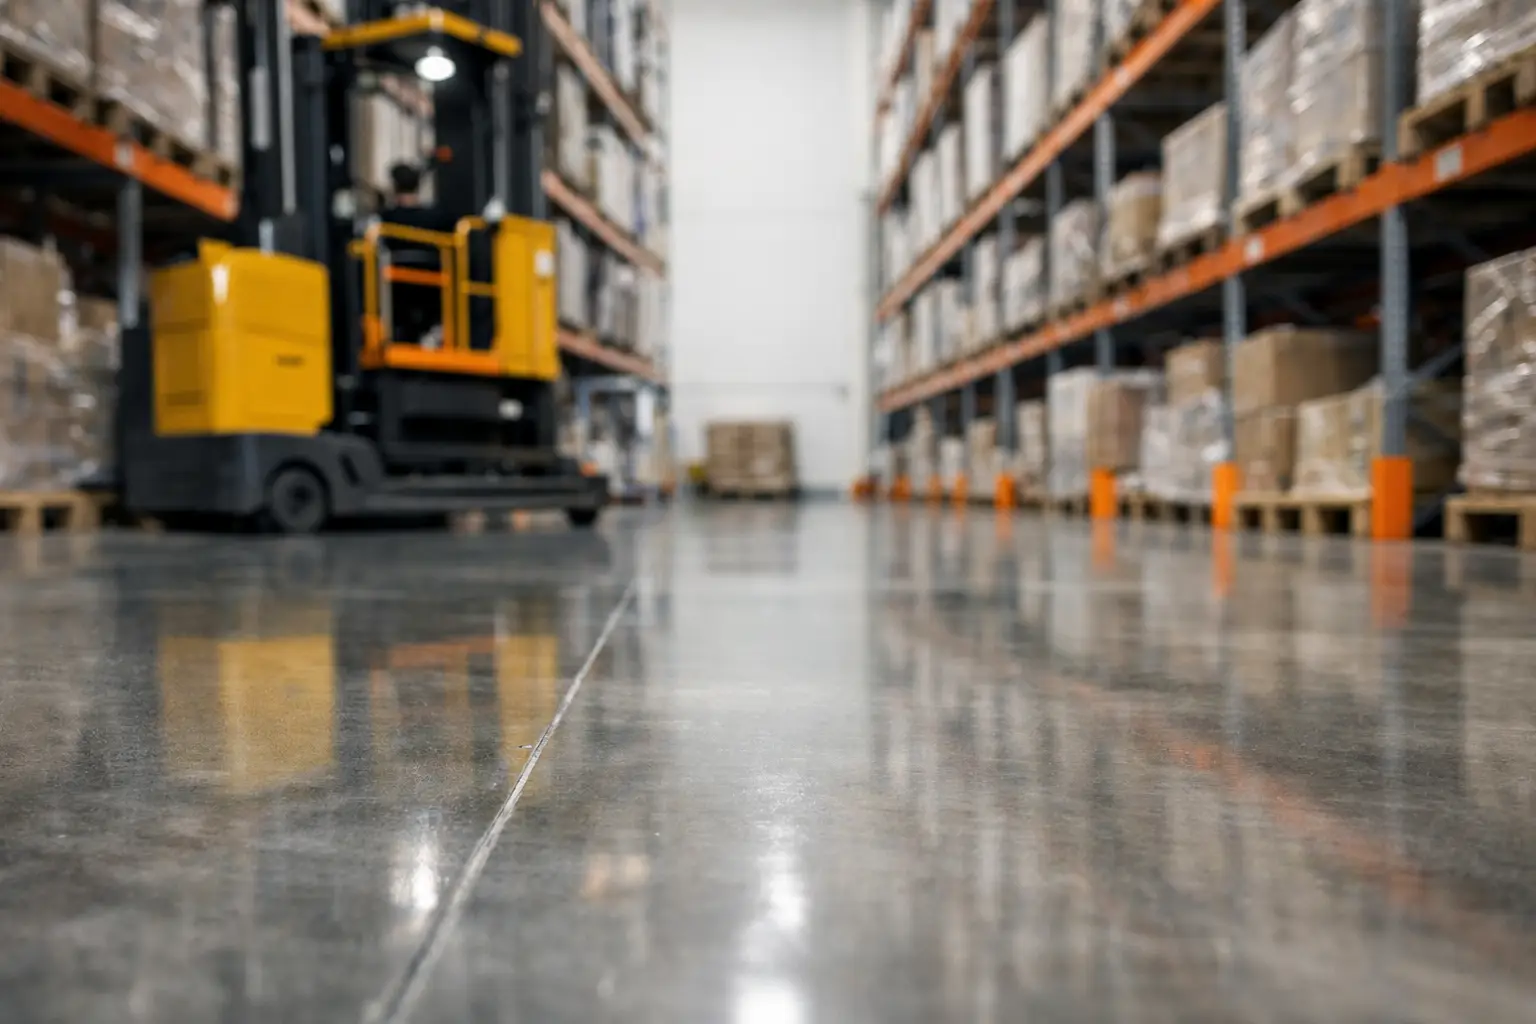
A very narrow aisle warehouse can have the right lift trucks, racking, controls, and operating plan and still underperform because of one foundational issue: the slab. VNA floor features determine how consistently a truck travels, how accurately it positions a pallet at height, and how much wear the operation places on equipment over time. In these facilities, flatness is not a finish detail. It is an operating requirement.
VNA trucks work in aisles that leave little room for correction. Their masts extend to significant heights, loads are handled close to rack structure, and travel paths are repeated thousands of times. Small surface variations that would be acceptable in a conventional warehouse can create mast sway, guidance issues, elevated wheel wear, and lower handling confidence in a VNA environment.
What Makes a VNA Floor Different?
A VNA floor is designed around defined truck wheel paths rather than general floor appearance alone. Its performance is measured in the direction the truck travels and across the aisle, with tolerances established for the equipment, rack height, guidance system, load profile, and operational duty cycle.
This distinction matters because a floor can appear flat to the eye yet fail to provide the local regularity required by a narrow-aisle truck. A broad floor profile may look acceptable across a bay while containing short-wave deviations that affect steer wheels, load wheels, or guidance components. At elevated lift heights, those deviations are amplified through the mast.
The primary objective is controlled, repeatable truck movement. That requires more than placing concrete to a general flatness number. It requires a floor design, installation method, testing plan, and repair strategy that all recognize the aisle as a precision travel corridor.
Defined-Direction Flatness
Conventional concrete floor specifications often rely on overall flatness and levelness values. Those values can be useful, but they do not always describe the floor behavior that matters most in a VNA aisle. Very narrow aisle operations need measurements that evaluate the truck path in its intended direction of travel.
Defined-direction testing identifies elevations and deviations along the wheel tracks and across the aisle width. The results help determine whether the surface will support the selected truck and racking configuration. This approach is especially relevant when trucks operate at high lift heights, where minor floor irregularities can become meaningful mast movement at the top pallet position.
The specification should identify the measurement method before construction begins. ASTM E1155 testing, F-number criteria, and defined-traffic tolerances can all be part of a project, but they are not interchangeable. The correct standard depends on the truck manufacturer’s requirements and the operational design of the warehouse.
Consistent Wheel Paths
VNA floor features must account for where the truck actually runs. The wheel paths are the highest-priority area because repetitive traffic concentrates there. Surface consistency along these lanes supports stable travel, predictable steering response, and reduced impact loading on wheels and truck components.
This is not simply a matter of achieving a smooth trowel finish. A smooth-looking surface may still contain localized highs, lows, edge defects, or transitions that disrupt a truck under load. The relevant question is whether the wheel path remains within the required profile tolerance over the specified measurement length.
Careful placing, screeding, finishing, curing, and verification all affect this result. So does access control during construction. Early traffic, poorly planned follow-on trades, and uncontrolled material storage can damage a precision slab before the warehouse is operational.
Joint Performance Is a Core VNA Floor Feature
Joints are necessary in many concrete slabs, but they are also a common source of long-term VNA floor problems. Every joint crossing introduces a potential change in elevation, support condition, and ride quality. Under repeated hard-wheel traffic, unprotected joint edges can spall, open, or lose load transfer.
A failed joint does more than look poor. It can produce a recurring impact point that affects operator comfort, truck maintenance, product stability, and floor deterioration. In narrow aisles, that impact is repeated on the same locations throughout every shift.
Joint layout should be considered with aisle geometry, not after it. Where practical, joints should be positioned to limit disruptive crossings in primary travel lanes. Their design should also address expected traffic, wheel loads, and the potential for slab movement. In some applications, jointless or long-panel solutions can reduce the number of crossings and improve the continuity of the truck route.
Where joints remain necessary, they require durable edge protection and timely maintenance. Repair materials must be selected for the operating environment, including traffic intensity, temperature conditions, cure requirements, and allowable downtime. A repair that is hard but poorly bonded, incorrectly profiled, or opened to traffic too soon will not deliver lasting performance.
Transitions Need the Same Precision
The beginning and end of a VNA aisle deserve the same attention as the aisle itself. Transitions at dock approaches, cross aisles, staging zones, door thresholds, ramp interfaces, and repaired areas can create abrupt changes in truck behavior.
These locations often receive mixed traffic and may experience more damage than the protected center of an aisle. A VNA truck entering a precision aisle from an uneven cross aisle carries that disturbance into the travel path. Level transitions and properly blended repairs help prevent this issue.
Surface Durability Supports Long-Term Accuracy
A VNA floor must retain its profile under traffic. Surface wear, cracking, curling, and localized settlement can gradually change a floor that initially met tolerance. Durability is therefore part of floor accuracy, not a separate concern.
Concrete mix design, slab thickness, reinforcement strategy, subbase condition, curing practice, and traffic timing all influence lifecycle performance. The right solution depends on the facility. A high-throughput distribution center with continuous turret-truck traffic has different demands than a lower-volume storage operation, even when both use narrow aisles.
Abrasion resistance is particularly relevant where hard polyurethane, steel, or high-load wheels repeatedly travel the same tracks. A weak or dusty surface can deteriorate quickly, creating roughness and reducing cleanability. In facilities with washdowns, chemicals, or specialized sanitation requirements, the floor system may also need protective treatments or coatings that preserve the required surface profile without creating a traction issue.
The trade-off is straightforward: a coating or overlay can solve a surface protection problem, but it must be compatible with the flatness requirement. Material thickness, installation tolerances, and transitions at the edge of the work area must be controlled. Applying a durable system without precision planning can introduce the very irregularities the VNA floor was meant to prevent.
Guidance Systems Change the Floor Requirements
Many VNA operations use wire guidance or rail guidance to keep trucks centered in the aisle. These systems improve travel control, but they do not eliminate the need for a precision floor. Guidance manages lateral positioning. The floor still governs vertical movement, ride quality, and the mast response caused by changes in elevation.
For wire-guided applications, the wire channel must be accurately located, properly cut, clean, and filled with a material suited to the traffic and operating conditions. Poor channel installation can leave low spots, weak edges, or incomplete bonding that becomes visible under repeated wheel loads.
The wire installation should be coordinated with final floor tolerances, racking layout, truck specifications, and testing procedures. Changes made in the field without that coordination can create misalignment issues that are expensive to correct after racks and equipment are in place.
Verification Should Happen Before Racking Is Installed
Once racking is erected and the warehouse is stocked, access for correction becomes limited and costly. VNA floor verification should occur early enough to allow practical remediation. That means establishing acceptance criteria before placement, measuring after construction, reviewing results by aisle, and addressing deficiencies before they become an operational constraint.
A disciplined process typically includes review of the truck manufacturer’s floor requirements, confirmation of aisle locations, defined-direction testing, and a documented plan for corrective work if results fall outside tolerance. The project team should also identify how repairs will be retested. A repair is not complete because it is visually acceptable. It is complete when it performs within the required profile.
For existing warehouses, floor surveying can identify whether issues are isolated to individual wheel paths, joints, cross aisles, or broader slab movement. This supports targeted grinding, joint repair, floor upgrade work, or localized reconstruction instead of defaulting to a larger and more disruptive scope.
Plan for the Operation, Not Just the Pour
The most effective VNA floor is specified around the actual operation: truck model, maximum lift height, loaded wheel configuration, rack clearances, travel frequency, guidance method, and maintenance expectations. Generic warehouse criteria can leave too much room for interpretation when the aisle is narrow and the loads are elevated.
Osis Group approaches superflat and VNA floor work as an operational system, where surface preparation, placement quality, joint strategy, wire guidance, and repair execution must perform together. That standard protects the investment in material handling equipment and helps facilities maintain reliable throughput.
Before committing to a new slab or corrective program, require the project team to define how the floor will be measured, accepted, and maintained. A precision aisle is built through accountable execution, then preserved through equally disciplined inspection and repair.


